
Wholesale Shell Egg Supply and Optical Grading

Kincade Farms Inc. supplies commercial shell egg inventory graded, packed, and refrigerated from our Lawrence County facility in Ravenden, Arkansas.

Commercial egg supply programs

Our commercial production serves food distributors, institutional food networks, and certified egg packing systems. We provide wholesale shell egg supplier arkansas services backed by active California Department of Food and Agriculture (CDFA) Registered Egg Handler credentials. We do not sell half-dozens to walk-in traffic or run roadside farm stands. Every shell egg transaction is a scheduled wholesale allocation packed to contract specifications.

Pricing across all shell egg tiers is inquiry-only. Commercial quotations are calculated from five operational variables: total lot volume in cases or pallets, selected egg grade tier, requested packaging format, freight terms (FOB Ravenden loading dock or refrigerated carrier delivery), and active buyer registration status. Lead times are quoted per commercial inquiry based on flock laying cycles and dock scheduling.

Commercial Shell Egg Grades

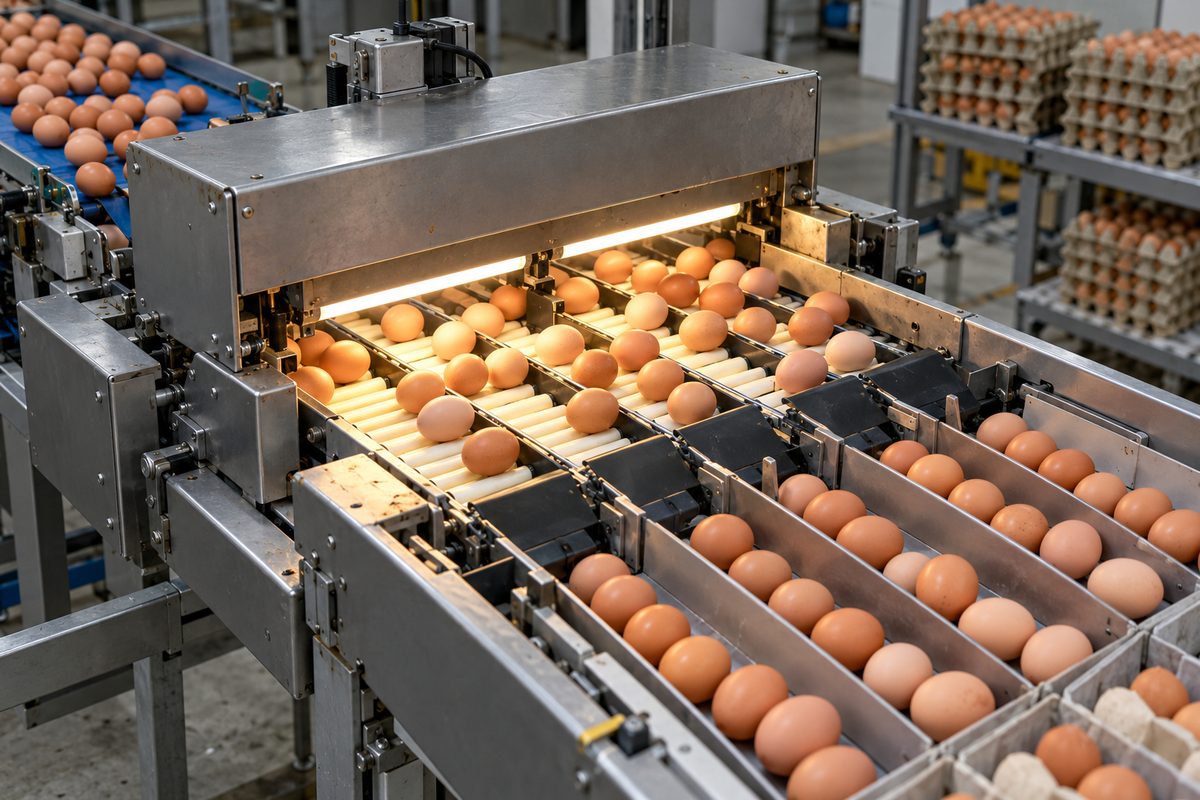
Every egg grade tier is processed through automated mechanical sorting lines and precision candling booths inside our Ravenden egg collection and packing facility.

Grade AA Large Shell Eggs

Grade AA Large eggs represent our highest mechanical sorting standard. Shells are clean, sound, and verified unbroken by acoustic and optical defect detection systems. The interior reveals firm, clear whites and high, centered yolks with an interior air cell depth not exceeding 1/8 inch. These lots are specifically designated for premium retail packaging and white-tablecloth food service distributors demanding flawless visual presentation.

Flock management and climate-controlled collection belts minimize cuticle disturbance. Eggs roll directly from automated house collection onto sanitized sorting channels without manual handling. Every lot is cooled to 45 degrees Fahrenheit within hours of oviposition to arrest internal degradation and preserve yolk index stability.
Shell Condition Clean & Intact Zero structural checks, stains, or micro-fractures allowed
Air Cell Depth ≤ 1/8 Inch Verified via backlit optical candling inspection
Packaging Modes Cases or Flats 15-dozen master packs or 30-dozen bulk corrugated cases
Price Basis By Inquiry Volume, packaging type, and freight terms determine rate

Grade A Large Shell Eggs

Our Grade A Large shell eggs provide consistent commercial performance for high-volume grocery distributors, institutional bakeries, and regional commissary kitchens. The shell is clean and practically normal with sound calcification. The interior egg white remains reasonably firm with an air cell depth between 1/8 inch and 3/16 inch, maintaining superior whipping, binding, and poaching characteristics under production kitchen demands.

Packaging configurations include 30-dozen corrugated master boxes stacked 30 cases per standard 48x40 wooden pallet, shrink-wrapped with corner boards for cross-country refrigerated freight stability. Pallet identification tags track exact laying barn ID, Julian packing date, and packing operator timestamps.

Minimum Weight 24 oz / Dozen Net weight verified on continuous electronic scale cells
Air Cell Depth ≤ 3/16 Inch Commercial grade standard meeting USDA & CDFA limits
Master Pack 30-Dozen Case Heavy-duty corrugated with moisture-resistant liners
Price Basis By Inquiry Determined by recurring contract commitments and lot counts

Pasture-Raised Contract Production

Kincade Farms Inc. operates pasture acreage structured to fulfill partner standards associated with Vital Farms pasture-raised specifications. Flocks access expansive, vegetated outdoor acreage adjacent to modernized shelter barns, promoting natural foraging behaviors, superior yolk pigmentation, and dense shell mineralization.

Pasture contract allocations are dedicated agreements established ahead of flock placement cycles. Each batch features segregated collection, optical sizing, and dedicated packing runs carrying full chain of custody paperwork under CDFA Registered Egg Handler oversight. We do not blend pasture lots with conventional production.

Pasture Access Vegetated Range Unrestricted daytime outdoor pasture runs with predator fencing
Standard Partner Vital Farms Specs Aligned with national certified pasture-raised criteria
Traceability Segregated Belts Flock-specific Julian date and pasture parcel tracking
Price Basis By Inquiry Scheduled annual or seasonal flock allocation contracts

Bulk Unwashed Nest-Run Lots

For regional breaking facilities, pasteurized liquid egg plants, and industrial food ingredient processors, Kincade Farms Inc. provides bulk shell eggs wholesale in unwashed nest-run format. Nest-run eggs are collected directly from automated housing belts, inspected for gross defects, and transferred directly into heavy-duty plastic transport flats without mechanical washing or chemical sanitization.

Transfer occurs on heavy plastic pallets ready for immediate refrigerated reefer staging. Outgoing bills of lading document farm flock source, collection timestamps, and continuous cooling curves. Because nest-run lots bypass sorting and packaging lines, processor contracts benefit from reduced handling friction and expedited dispatch timelines.

Condition Unwashed / Natural Natural shell cuticle preserved for pasteurization plants
Handling Format Plastic Flats Sanitized commercial egg trays on reinforced pallets
Target Sector Egg Breakers Certified further-processing operations and liquid processors
Price Basis By Inquiry Quoted per hundredweight or bulk pallet transfer schedule
Stage 1 — Automated Collection

Poultry house collection belts

Freshly laid eggs move continuously along variable-speed longitudinal collection belts inside the poultry barns. The system transitions eggs smoothly to transverse cross-conveyors, preventing shell shock, hairline fissures, or manual touching.

Continuous belt Zero human touch
Stage 2 — Optical Sorting & Grading

Optical defect rejection

Shell eggs enter the grading facility where optical sensors, acoustic crack detectors, and high-intensity candling units evaluate exterior soundness and interior yolk condition. Sub-standard eggs are ejected automatically.

Acoustic sensor Optical candling
Stage 3 — Packaging & Case Packing

Automated robotic packing

Graded eggs pass to automated packing arms that position eggs large-end-up into pulp flats and corrugated master containers. Lot labels are printed and adhered instantly with date, house number, and CDFA registration codes.

CDFA lot stamped Master cases
Stage 4 — Refrigeration & Staging

Cold-chain quarantine dock

Cased eggs are palletised, stretch-wrapped, and transferred into cold staging rooms held continuously at or below 45 degrees Fahrenheit (7.2 degrees Celsius). Digital temperature recorders track ambient conditions until trailer dispatch.

≤ 45°F locked Pre-cooled trailers
Commercial shell egg processing line in Lawrence County Arkansas.
Continuous egg handling infrastructure: collection to refrigerated dock.

Commercial Buyer Objections Answered

Egg purchasers manage volatile markets and strict sanitary enforcement. Here is how Kincade Farms Inc. addresses practical commercial hurdles:

“Every pallet leaving our Ravenden dock carries verified internal candling data, cold-chain temperature logs, and active CDFA registration numbers.”
Kincade Farms Inc. Lawrence County Facility • Ravenden, AR CDFA Valid Thru 12/31/2026

Schedule Commercial Supply Intake

Contact our Ravenden dispatch office to confirm lot allocations, optical grading tiers, and scheduled freight transport windows.